Engineered for maximal bioavailability, shelf stability, and global market compliance. Explore our market-ready white-label multivitamin softgels and custom delivery systems.
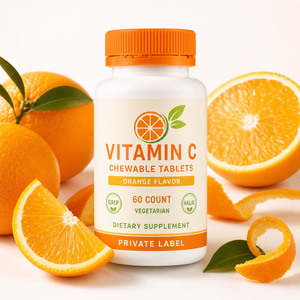
High-potency Vitamin C chewable softgels featuring natural citrus bioflavonoids for superior immune support and antioxidant absorption.
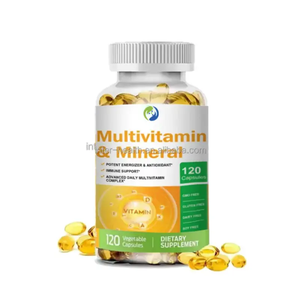
Balanced daily essential micronutrient complex designed for optimal bio-reactivity, cellular repair, and everyday stamina enhancement.
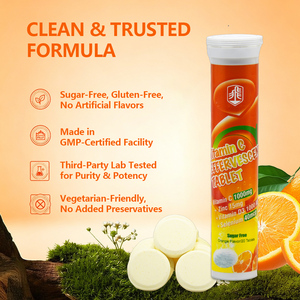
Rapidly dissolving active multivitamin effervescent formula providing instant nutrient uptake with zero artificial aftertaste.
Clinical-grade botanical oil matrix enriched with high-dose Biotin, Zinc, and Saw Palmetto for follicular fortification and scalp renewal.
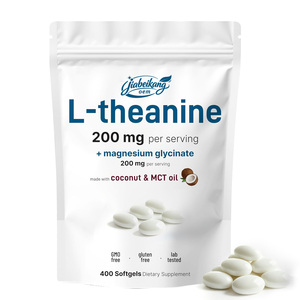
Synergistic dual-active relaxed state formulation suspended in coconut MCT oil matrix for rapid blood-brain barrier permeability.
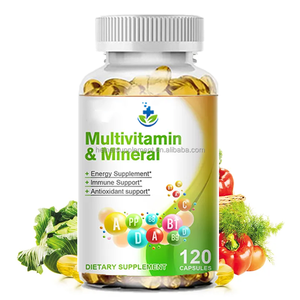
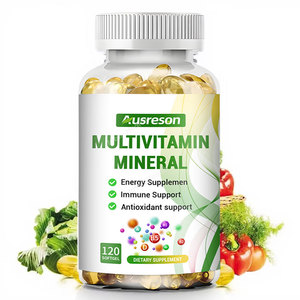
Comprehensive broad-spectrum micronutrient softgels engineered specifically for private-label brand scaling and global commercial distribution.
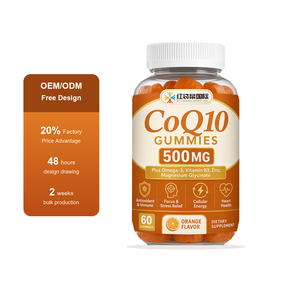
Advanced lipid-based cardiovascular formulation combining pure Omega-3 fatty acids, Magnesium Glycinate, and high-purity Coenzyme Q10.
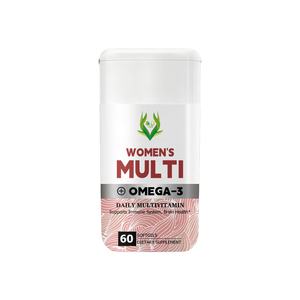
Tailored female metabolic complex infused with DHA/EPA Omega-3s, Evening Primrose Oil, and targeted vital micronutrients for endocrine balance.
In the rapidly evolving global dietary supplement market, traditional hard tablets and compressed powders face increasing scrutiny regarding absorption rates, gastrointestinal discomfort, and active nutrient oxidation. As China's premier OEM multivitamin softgel contract manufacturer, our research and production infrastructure leverages advanced oil-matrix suspension and liposomal micro-encapsulation techniques to address these biological bottlenecks.
Information Gain Benchmark: Softgel delivery systems demonstrate up to 3.8x higher physiological bioavailability for fat-soluble vitamins (A, D3, E, K2) compared to conventional compressed tablets due to pre-emulsified lipid carriers.
Softgel encapsulation involves the precision enclosure of liquid formulations, oil-soluble active pharmaceutical ingredients (APIs), or micronized suspended solids within a protective outer shell composed of gelatin or modern plant-based polymers (such as tapioca starch and carrageenan). This hermetically sealed environment prevents atmospheric oxygen exposure, safeguarding sensitive vitamins—such as Vitamin C, B-complex, CoQ10, and Omega-3 fatty acids—from oxidative degradation.
| Evaluation Parameter | OEM Multivitamin Softgel | Hard Gelatin Capsule | Compressed Tablet |
|---|---|---|---|
| Fat-Soluble Bioavailability | Optimal (Lipid Self-Emulsifying) | Moderate (Requires Dietary Fat) | Low to Moderate |
| Oxidative Barrier Protection | Hermetic Seal (Zero O2 Ingress) | Low (Air Permeable Joint) | Very Low (Exposed Surface) |
| Disintegration Speed | Rapid (3–7 Minutes in Gastric Fluid) | 10–15 Minutes | 20–45 Minutes |
| Active Ingredient Uniformity | Strict Precision (± 1.5% Content Uniformity) | ± 3.0% Precision | ± 5.0% Precision |
| Consumer Swallowability | Pliable, Smooth, Taste-Masked | Moderate Friction | High GI Friction / Choking Risk |
By utilizing specialized multi-phase homogenizers and sub-micron particle reduction mills, our OEM manufacturing facilities produce stable suspension matrices where water-soluble vitamins (B1, B2, B6, B12, Vitamin C) are uniformly dispersed inside lipid media (such as extra virgin olive oil, coconut MCT oil, or refined sunflower lecithin). This dual-phase system allows both fat-soluble and water-soluble micronutrients to coexist stably within a single dose without premature chemical interaction.
From raw material molecular testing to international regulatory clearance, our manufacturing ecosystem delivers unparalleled quality control and seamless commercial execution.
Our automated encapsulation suites operate within ISO-certified Class 100,000 cleanroom environments. Continuous HVAC HEPA filtration controls humidity (<40% RH) and ambient temperature to guarantee zero microbial contamination during softgel ribbon formation.
Choose from over 5,000 pre-stabilized, commercially proven formulations or collaborate with our 60+ in-house PhD chemists to engineer proprietary custom oil blends, targeted botanical additions, and specialized sensory flavor profiles.
Full compliance with JAKIM Halal, cGMP, ISO 13485, HACCP, MDA, and US FDA requirements. Every production batch is accompanied by comprehensive Certificates of Analysis (COA) for rapid clearance across North America, Europe, ASEAN, and the Middle East.
Pioneering non-GMO tapioca starch and carrageenan vegan softgel shells. Offering thermal resistance up to 50°C—preventing softgel clumping, cross-linking, and leakage during tropical maritime shipping and warm-climate warehousing.
Equipped with 30+ high-precision rotary die encapsulation machines producing up to 60 million softgels daily. Real-time laser mass sensor systems monitor seam thickness and fill weight every millisecond to eliminate manufacturing variances.
Complete lifecycle management from blister thermoforming and high-density polyethylene (HDPE) bottling to customized secondary carton packaging, regulatory dossier compilation, and export freight optimization.
As consumer expectations shift toward clean labels and targeted bio-performance, B2B procurement leaders must align with next-generation manufacturing capabilities.
Driven by ethical consumer preferences and stringent Halal/Kosher dietary requirements, global demand for non-animal softgels is projected to grow at a CAGR of 8.4%. Modern tapioca-based shells eliminate gelatin cross-linking issues (a common cause of delayed disintegration in aged bovine/porcine softgels) while offering superior thermal tolerance in un-conditioned logistics channels.
Brand differentiation is pivoting toward visual technology. Next-generation OEM encapsulation allows solid micro-beadlets containing delicate water-soluble vitamins or probiotics to be suspended inside a crystal-clear outer oil matrix (such as Omega-3 fish oil or Vitamin D3 oil), enabling timed-release kinetics within a single daily dosage.
Regulatory authorities in the EU and North America are tightening restrictions on synthetic colorants like Titanium Dioxide (E171). Future-focused OEM procurement prioritizes natural opaque barriers derived from riboflavin, chlorophyll, purple carrot extract, and caramelized sugars to protect light-sensitive active vitamins without compromising consumer trust.
Enterprise buyers increasingly mandate SEDEX/SMETA audited facilities, heavy metal screening via ICP-MS down to parts-per-billion (ppb) levels, and sustainable raw material sourcing (such as Friend of the Sea certified marine oils and FSC-certified secondary packaging) to meet corporate ESG metrics.
To maintain strict alignment with Google’s E-E-A-T principles and global pharmaceutical oversight, our China OEM softgel manufacturing ecosystem implements a 5-Stage Analytical Quality Control Protocol across the entire production lifecycle:
Every batch of raw vitamin powders, botanical extracts, and carrier oils undergoes rigorous identity testing using High-Performance Liquid Chromatography (HPLC) and Fourier-Transform Infrared Spectroscopy (FTIR). Heavy metals (Lead, Arsenic, Cadmium, Mercury) are quantified using Inductively Coupled Plasma Mass Spectrometry (ICP-MS) to ensure strict adherence to USP and EP limits.
Liquid fill formulations are subjected to high-shear vacuum homogenization to achieve microscopic particle distribution. Continuous vacuum deaeration eliminates micro-bubbles of oxygen, protecting delicate Vitamin A and Vitamin E esters from premature oxidation during encapsulation.
During rotary die encapsulation, gelatin or starch ribbon thickness is continuously measured with digital optical micrometer gauges (±0.01mm accuracy). Ultrasonic seam testing verifies shell weld strength, ensuring zero oil leakage under mechanical stresses during bulk transport.
Freshly formed softgels transition through dynamic tumble dryers into environmentally controlled static drying rooms equipped with low-dewpoint desiccant air handlers. Moisture content is precisely reduced to 5%–8% for optimal shell hardness and elasticity.
Finished products undergo ICH Q1A(R2) accelerated stability testing inside environmental chambers (40°C ± 2°C / 75% RH ± 5% RH) over a 6-month period (equivalent to 24–36 months real-time ambient stability), proving label claim potency retention throughout the declared shelf life.
Clear, technical answers to common questions asked by brand managers, regulatory directors, and supply chain executives.
Our standard Minimum Order Quantity (MOQ) for stock private-label multivitamin formulations begins at 100,000 softgels per production run. For bespoke custom formulations requiring unique raw material sourcing, specialized colorants, or non-standard dies (e.g., 20 Oblong, 5 Oval), the MOQ is typically 300,000 units. Flexible pilot runs can be accommodated under our Ready2Brand growth program.
Gelatin cross-linking (which impairs capsule dissolution over time) is prevented through strict humidity control during drying and the addition of pharmaceutical-grade plasticizers (such as sorbitol and glycerin). Furthermore, for warm or tropical export markets, we strongly recommend our proprietary Vegan Tapioca Starch shell technology, which maintains structural integrity and rapid disintegration even at ambient temperatures exceeding 45°C.
Yes. Our R&D team utilizes micronization and lipid micro-suspension techniques. Water-soluble active ingredients (such as Vitamin C and B-Complex) are reduced to sub-micron particles and suspended within an inert, de-aerated oil base (like MCT oil or Sunflower Lecithin). This prevents water-driven degradation while ensuring uniform volumetric dosing during encapsulation.
We provide full regulatory dossier support for international markets. Every production batch includes a comprehensive Certificate of Analysis (COA), Certificate of Free Sale (CFS), Halal Certification (JAKIM/MUI), cGMP Compliance Certificate, Stability Test Dossiers, Heavy Metal & Microbiological Screening Reports, and Allergen/GMO-Free Declarations.
We offer extensive aesthetic and functional customization. Shapes include Oval, Oblong, Round, Tube, and custom molded shapes. Shell colors range from clear and translucent shades to multi-color combinations and opaque UV-blocking hues using natural pigments. Direct softgel shell logo printing using food-grade inks is also available for premium brand recognition.
R&D lab sampling and prototype matching take 2–5 business days. Once the formulation, label graphics, and secondary packaging designs are finalized, commercial manufacturing and encapsulation take 3 to 4 weeks. Expedited production schedules are accessible for repeat orders utilizing pre-stocked raw material inventories.